Full Technical Guide
Aggregate moisture probe errors are one of the fastest ways to lose control of total batch water in a concrete plant. When the probe drifts, is installed in a poor location, is coated with fines, or is calibrated against an unrepresentative sample, the batching controller can add too much or too little water even though the programmed mix design is correct. The result may be unstable slump, inconsistent workability, avoidable water corrections, variable yield, and unnecessary troubleshooting downstream.
This guide explains how to diagnose and calibrate an aggregate moisture probe in a concrete batching plant without treating the sensor reading as the only source of truth.
Why aggregate moisture measurement matters
Concrete aggregates carry variable water into every batch. The plant controller must distinguish between water already present in the aggregates and water that still needs to be added at the mixer. This is particularly important for fine aggregate, where moisture can change quickly with rain, stockpile drainage, reclaim water, covered storage conditions, or a new delivery.
A moisture probe is therefore not just a display instrument. Its signal affects the plant’s water compensation logic. If the measured moisture is wrong, the calculated free-water contribution from the aggregate is also wrong.
Microwave moisture sensors are widely used for this duty because they can measure material continuously in bins, hoppers, chutes, or mixers. Sensor manufacturers emphasize that the instrument must see a representative and repeatable flow of material, not an unusual pocket of wet or dry aggregate. Hydronix describes microwave moisture measurement as a process-control tool for concrete and bulk materials.
Typical signs that the moisture probe may be wrong
- Slump changes even though the recipe and weighed materials have not changed.
- The operator repeatedly adds manual water after batching.
- The probe value is nearly constant while the stockpile condition is visibly changing.
- The reading jumps sharply when the feeder starts or stops.
- Moisture compensation appears reasonable for one aggregate source but not after a source change.
- Laboratory moisture tests and the online reading show a persistent difference.
- The first batch after a long stop behaves differently from later batches.
- The sensor shows unstable values when the material level in the bin becomes low.
None of these observations alone proves that the probe is defective. A wrong slump can also come from admixture dosage, cement temperature, aggregate grading, mixer condition, weighing error, or incorrect batching sequence. When investigating quality variation, compare the moisture diagnosis with the plant’s concrete strength and quality-control records rather than treating one signal in isolation. The correct approach is to isolate the measurement system before replacing hardware.
Step 1: Check the installation before recalibrating
Do not start by changing calibration constants. First inspect the mechanical installation.
Confirm that the sensor sees representative material
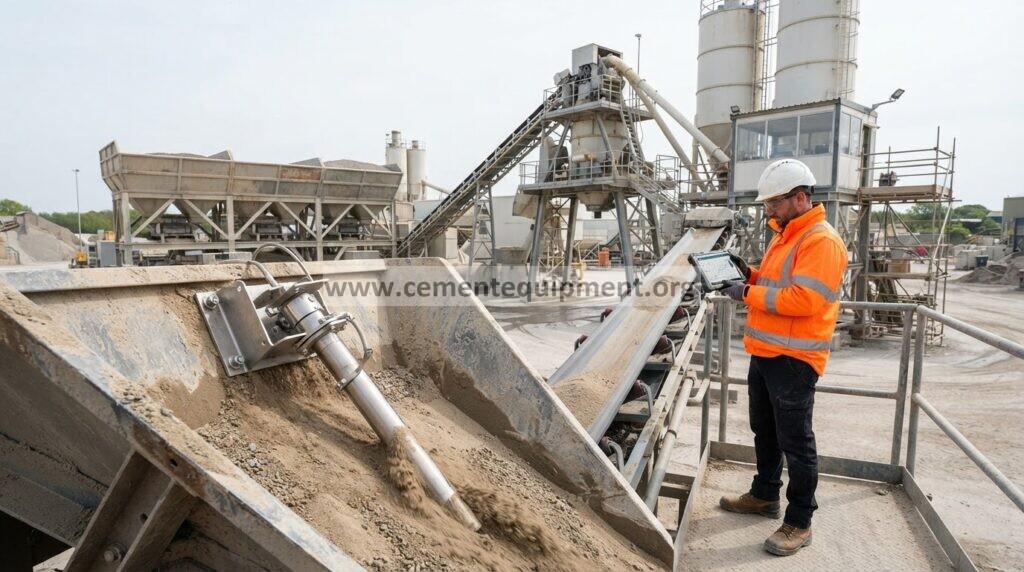
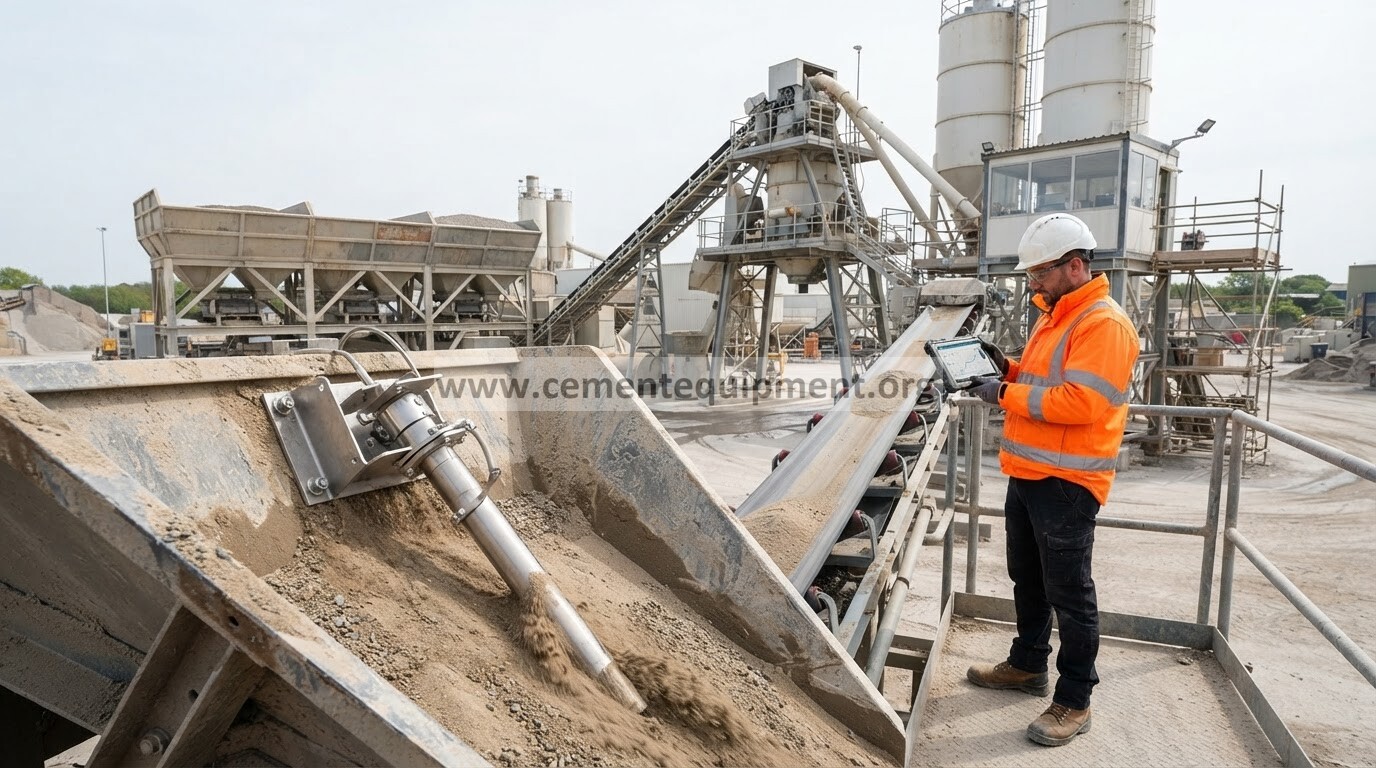
The sensing face should remain in consistent contact with the aggregate stream or stored material. Empty pockets, bridging, segregation, direct impact from large particles, or a changing bed depth can produce unstable readings. If the probe is mounted in a sand bin, compare the reading when the bin is normally loaded with the reading near low level. A large systematic shift may indicate that the installation geometry is influencing the measurement.
Inspect the sensing face
Build-up can make a healthy sensor appear inaccurate. Hardened fines, cementitious contamination, clay, or compacted wet sand around the face can create a measurement condition different from the flowing bulk material. Clean the probe using the manufacturer’s approved method and inspect for wear or damage.
Check cables, grounding and connectors
Intermittent wiring, damaged shielding, poor grounding, water ingress, or loose connectors can create noise that looks like process variation. Trend the raw sensor signal if the controller exposes it. Random spikes suggest a different problem from a stable but consistently biased reading.
Step 2: Verify the actual aggregate moisture independently
The online reading must be compared with a representative physical sample. The sample should be taken as close as practical to the material measured by the probe and at approximately the same time.
Use the plant or laboratory’s approved reference moisture method. The objective is to establish the actual moisture content of the material independently of the online sensor. A single grab sample may be misleading if the stockpile or bin is strongly segregated, so repeat the comparison under more than one moisture condition whenever possible.
A useful diagnostic record contains:
| Check | Record |
|---|---|
| Online probe | Displayed moisture and raw signal, if available |
| Reference sample | Measured moisture from the plant/lab method |
| Aggregate | Source, size/fraction and bin number |
| Plant condition | Bin level, feeder running/stopped, recent rain or delivery |
| Concrete response | Observed workability/slump trend and any manual water correction |
Step 3: Decide whether the problem is offset, slope or process variation
Stable offset
If the probe follows moisture changes correctly but remains consistently above or below the reference result, the problem may be a calibration offset or material-specific calibration issue.
Wrong sensitivity or slope
If the sensor is close at low moisture but increasingly wrong as the material gets wetter, a multi-point calibration may be required. Do not force one calibration point to correct the entire range.
Poor repeatability
If identical-looking process conditions produce very different readings, investigate installation, electrical noise, material flow, segregation, or sensor condition before recalibrating. Calibration cannot correct a signal that is not repeatable.
Step 4: Recalibrate using representative conditions
Follow the sensor manufacturer’s procedure and use samples that represent the aggregate actually being batched. Avoid calibrating immediately after an unusual event such as a fresh delivery with strongly segregated moisture unless that condition represents normal operation.
For a useful calibration:
- Stabilize the normal material flow and sensor contact.
- Record the online reading.
- Take a representative aggregate sample near the measurement point.
- Determine reference moisture using the approved plant/lab method.
- Repeat at additional moisture conditions if the sensor procedure supports multi-point calibration.
- Enter or update calibration values according to the sensor/controller instructions.
- Recheck with a fresh sample rather than validating against the same sample used to create the calibration.
General batching-plant calibration guidance also treats the moisture probe as a separate calibration item because moisture compensation directly affects water dosing. MEKA’s batching-plant calibration guide specifically notes the need to calibrate aggregate moisture probes independently.
Step 5: Verify the controller’s moisture-compensation logic
A correctly calibrated probe can still produce bad concrete if the batching controller interprets its value incorrectly. Confirm whether the controller is using total moisture, free moisture, or another configured basis, and verify how aggregate absorption is represented in the mix data.
Also check that the correct sensor is mapped to the correct aggregate bin. This sounds simple, but control-system edits, bin reassignment, or recipe changes can create a mismatch where a valid sensor signal is applied to the wrong material.
After any calibration change, verify the complete calculation chain:
measured aggregate moisture → calculated water carried by aggregate → corrected added water → actual concrete response.
Common root causes and corrective actions
| Symptom | Likely cause | Recommended check |
|---|---|---|
| Reading stuck or unusually flat | Build-up, poor contact, configuration or failed signal | Inspect sensor face, raw signal and wiring |
| Large random spikes | Electrical noise, intermittent cable, unstable material contact | Check shielding, connectors and material flow |
| Consistent bias versus lab test | Calibration offset or changed aggregate characteristics | Repeat reference samples and recalibrate if confirmed |
| Error grows as material gets wetter | Calibration slope not representative | Use multiple representative moisture points where supported |
| Good sensor reading but wrong slump | Controller logic or another batching variable | Audit water correction, admixture, weighing and mixer sequence |
| Reading changes with bin level | Installation geometry or inconsistent sensor coverage | Inspect probe location and material contact |
Do not use slump alone as the calibration reference
Concrete response is valuable as a cross-check, but slump should not be treated as a direct moisture meter. Workability is influenced by many variables. A patent describing aggregate-moisture monitoring in concrete production illustrates the value of comparing probe information with monitored concrete behavior, but the strongest field practice is still to verify the sensor against a direct moisture reference and then use concrete behavior as an additional diagnostic signal rather than the only calibration basis.
Practical maintenance checklist
- Inspect the sensing face for build-up and wear.
- Check cable condition, grounding and connector sealing.
- Trend the moisture value instead of judging one instantaneous reading.
- Compare online readings with reference samples periodically and whenever aggregate source or condition changes materially.
- Revalidate after sensor replacement, controller replacement, bin reassignment, major maintenance or aggregate-source changes.
- Keep calibration records so gradual drift can be separated from sudden failure.
- After calibration, verify actual batch-water correction and concrete response.
Final diagnostic rule
When a concrete batching plant shows unexplained water or slump variation, do not immediately blame the probe and do not immediately change its calibration. First confirm installation, repeatability, independent moisture reference, calibration fit, controller mapping and water-correction logic. That sequence prevents a control-system problem from being hidden by an unnecessary sensor adjustment.
For engineers working on concrete batching, process control, maintenance and quality systems, Infinity for Cement Organization maintains a broader technical resource library covering cement and concrete production, equipment and troubleshooting. Explore the engineering resources at cementequipment.org.