A rotary kiln is the rotating high-temperature reactor that converts cement kiln feed into clinker. Cement plants use wet, semidry/Lepol, long dry, suspension-preheater and precalciner kiln systems, with the modern choice driven mainly by feed preparation, heat recovery, production rate and fuel efficiency.
Understanding Rotary Kiln Types
Quick answer: In cement manufacturing, a rotary kiln is a slightly inclined, refractory-lined rotating cylinder that heats prepared raw meal until clinker minerals form. The main process configurations are wet, semidry/Lepol, long-dry, suspension-preheater and precalciner kilns. Modern plants generally favor preheater/precalciner systems because much of the heating and calcination occurs before material enters the rotary tube.
Related process references: cement manufacturing process, cement chemistry and types of cement, and the rotary kiln design calculations guide.
Each type of rotary kiln has its own advantages, such as the wet process kiln's ability to blend feed more uniformly, and the semidry process kiln's efficiency in fuel consumption.
Types of Rotary Kilns
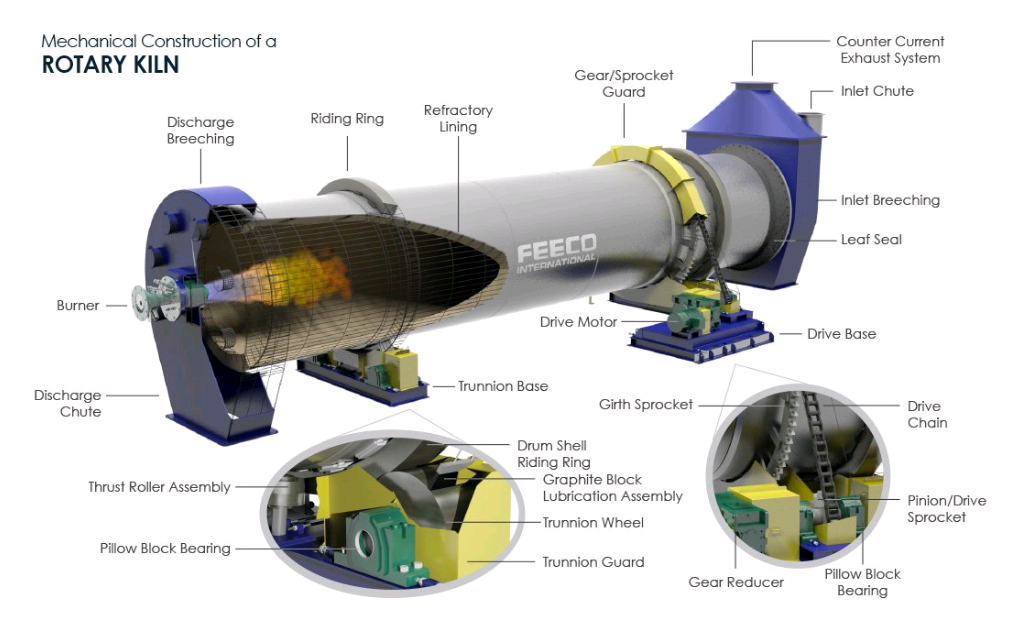
For cement clinker production, the main rotary-kiln process configurations are:
- Wet-process kiln — slurry feed enters the kiln with high moisture.
- Semidry / Lepol kiln — pelletized or filter-cake feed is partly heated or calcined on a grate before entering the kiln.
- Long dry kiln — dry powder feed is heated inside a long rotary kiln.
- Suspension-preheater kiln — cyclone stages recover kiln-exit heat before feed enters the rotary kiln.
- Precalciner kiln — a separate firing stage performs much of the calcination before material reaches the kiln burning zone.
The sections below explain how each arrangement works and where its main operating trade-offs come from.
Rotary kiln types: quick engineering comparison
| Kiln system | Feed / heat-recovery arrangement | Main engineering implication |
|---|---|---|
| Wet process | Slurry feed; water is evaporated in the kiln | Long kiln and high evaporation heat duty; useful mainly as an existing/legacy configuration. |
| Semidry / Lepol | Pelletized/filter-cake feed preheated on a grate | External heat recovery shortens the rotary section but adds grate-system operating requirements. |
| Long dry | Dry feed; much of the heating occurs inside the kiln | Long shell and relatively hot exit gas; chain systems may be used for heat recovery. |
| Suspension preheater | Cyclones recover kiln-exit heat before feed enters the kiln | Shorter rotary section and better heat recovery; volatile cycles and preheater pressure-drop/blockage become important. |
| Precalciner | Substantial fuel input and calcination occur before the rotary kiln | High-throughput modern arrangement; kiln, calciner, tertiary-air and cooler performance must be treated as one pyroprocess system. |
Do not select or benchmark a kiln from type alone. Throughput, raw-material burnability and moisture, fuel characteristics, bypass requirement, clinker quality, cooler/preheater configuration, retention time and mechanical support arrangement all matter. Modern OEM designs also differ mechanically: two-support and three-support kilns, drive arrangements, tyres/support rollers, seals and axial-thrust systems are design-specific.
Comparing preheater and precalciner configurations? Review the cyclone preheater and precalciner engineering guide for gas–solid heat exchange, cyclone pressure drop and calcination considerations. Equipment-specific design and operating limits still require OEM and plant data.
Engineering next step: check the kiln retention-time formula and worked calculation, then use the free kiln residence-time calculator. For dimensions, loading and design checks, continue to the rotary-kiln design calculations.
WET PROCESS
Into this group fall all processes in which the kiln feed enters the kiln in the form of a slurry with a moisture content of 30 to 40%. In comparison with a dry-process kiln of the same diameter, a wet-process kiln needs an additional zone (dehydration zone) to drive off the water from the kiln feed. Therefore, it must be considerably longer in order to achieve the same production rate.
To produce an equivalent amount of clinker, a wet-process kiln requires theoretically more .fuel than a dry-process kiln because of the extra heat required to evaporate the water. However, in actual operation of a kiln this fundamental fact does not always hold entirely true. As one progresses in the reading of this book, the reasons for these discrepancies between theory and actual operation will become clearer and understandable.
Advantages of a wet-process kiln are:
- feed is blended more uniformly than in the dry process
- dust losses are usually smaller, and
- in moist climate regions, wet processing of the raw material is more suitable than dry because of moisture already present in the blend materials.
SEMIDRY PROCESS
This member in the group of rotary kilns is also widely known under the term Grate Process Kiln or Lepol Kiln. The thermal performance of semidry/Lepol kilns depends on feed moisture, grate heat recovery, plant capacity and operating conditions. Do not assume fuel consumption matches a modern suspension-preheater/precalciner kiln; compare measured specific heat consumption on a consistent clinker-production basis. Output rates, however, lag behind the aforementioned types of kilns. However, it is advantageous to select a Grate Process Kiln over a preheater or precalciner kiln in places where raw material moisture is so high that it cannot be economically dried by waste heat from the kiln. Lepol Kilns, because of the fact that the kiln exit gases pass through the granular feed bed, operate with much lower dust contents in the waste gases which gives these kilns a decisive advantage over other preheater kilns. Instead of granulating the kiln feed, some plants use filter press cakes to feed the kiln. In such cases, the wet-kiln feed slurry is first passed through large presses for removal of the free water and more importantly, to remove alkalies before the filter cakes are fed to the kiln.
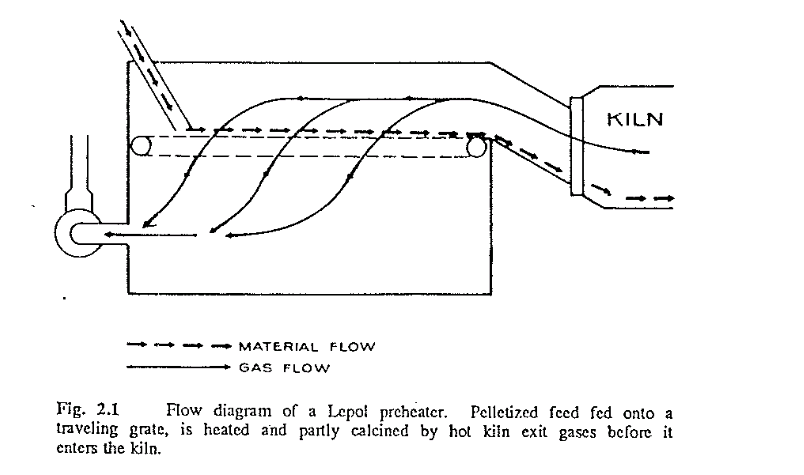
In the grate process, pulverized dry-kiln feed is first pelletized into small nodules by means of 10-15% water addition, then the nodules are fed onto a traveling grate where they are partly calcined before they enter the rotary kiln. Heating of the nodules is effected by the exit gases from the rotary kiln, the hot gases passing through the material bed from above as they are drawn downward through the grates by means of a fan. The partly calcined material then falls down a chute into the rotary kiln where final clinkerization takes place. Because the kiln feed is already partly calcined before it enters the kiln, the rotary kiln itself is only about one-third the usual length. Fig. 2.1 is a schematic diagram of the flow of gas and material through a Lepol grate-process preheater.
One advantage of grate-process kilns is the uniform size of clinker leaving the kiln, an aspect that is decidedly beneficial for grinding the clinker. However, there are some features not found in conventional rotary kilns that need very close attention; for example, production of the nodules and control of the thickness of the feed bed over the traveling grates. Such a kiln usually requires additional labor to attend the granulator plant.
DRY-PROCESS KILNS
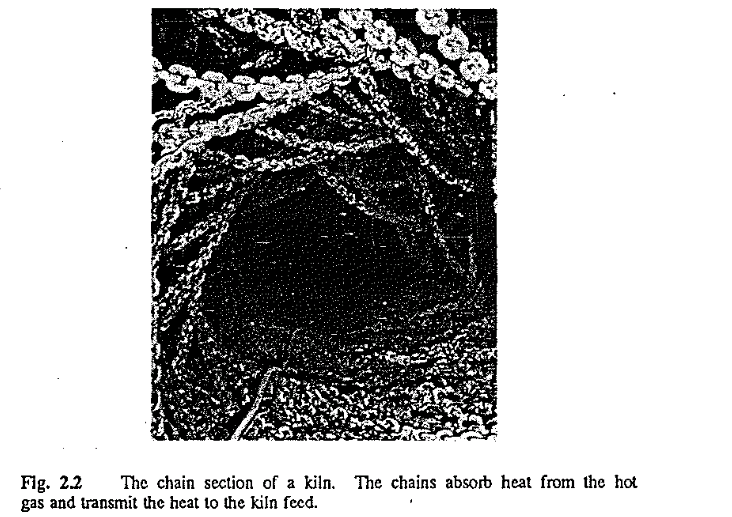
As the term indicates, in this process the kiln feed enters the kiln in dry powder form. Dry-process kiln dimensions are similar to wet kilns in that they are long and typically show a length-to-diameter ratio of approxi mately 30:1 to 35:1. Long dry-process kilns can have relatively hot exit gases. Whether gas conditioning, cooling, or heat recovery is needed depends on the actual gas temperature, dust-collection equipment and plant design; water spraying at the kiln feed end is not a universal requirement. Most dry kilns are equipped with chain sections at the feed end to transfer heat, that other wise would be lost, to the feed before the gases leave tl1e kiln.
Fig. 2.2 shows a picture of a chain section. The gases enter the chains at a temperature of approximately 800 C (1470 F) and leave tl1e kiln exit at a temperature of 450 C (840 F). In countercurrent flow, the material enters the chains with a temperature of 50 C (120 F) and emerges from the chain section with a temperature of 730 C (1350 F). Chain sections, where fitted, require inspection and maintenance, but they are not an absolute requirement for all dry-process kiln designs. Because of the high costs of these chains, there is a tendency in many plants to neglect proper and frequent maintenance. How ever, i_t has been found in many instances that the costs saved, by not tak ing care of the chain system, are coming back manyfold in the form of higher fuel operating costs.
Some long dry kilns have high-temperature exhaust suitable for evaluation as a waste-heat source. Feasibility depends on available heat, gas conditions, existing process heat use and project economics; waste-heat recovery is not unique to long dry kilns. As a matter of fact there are several plants with dry kilns that generate their own power and many existing plants are taking a hard look at the feasibility of adding a power plant to their facility. The reasoning is simply that generating power is energy-conserving and in some locations it may be more economical to add a power plant to an existing dry kiln than to convert this kiln to preheater status.
THE PREHEATER KILN
In the gas-suspension preheater kiln, the dry feed is preheated and partly calcined by the hot kilh exit gases in a tower of heat exchange cyclones. This concept is, contrary to popular beliefs, not new because a patent on this type of kiln was issued in Czechoslovakia already in the early 1930’s. However, the suspension preheater kiln as it is known today did not come into its own right until after World War II when German kiln manufacturers were able to overcome the operational and structural problems of these types of kilns (Fig. 2.3).
The preheating of the kiln feed is done outside the rotary kiln proper, i.e., before the feed enters the kiln. The heat exchange between the gas and the material takes place in the cyclones while both are in suspension. Many different designs of preheater towers are in existence using this basic principle. The most common design is the parallel four-stage preheater. Some of these can reach output rates of up to 8000 metric tons per day. Exit gas temperatures leaving the top # 4 stage are around 340 C (640 F) and in many such plants, these waste gases are used (together in some cases with tile waste gases from the clinker cooler) for drying and preheating of kiln feed in the raw grinding department. One drawback of preheater kilns is the high concentration of volatile constituents such as alkalies, sulfur, and chlorides in the kiln exit gases that give tise to numerous plug-up problems at the lower cyclone stage and kiln inlet. A kiln-gas bypass is not a universal requirement for suspension-preheater kilns. Its need and design depend on the chloride, sulphur and alkali inputs from raw materials and fuels, their internal circulation, clinker-quality constraints, and the plant’s measured build-up or blockage history. A gas bypass can be effective for limiting chloride cycles, but its removal of sulphur and alkalis is more limited; it also creates dust and thermal losses that require engineering assessment. See the ECRA technical review of sulphur and chloride cycles.
Specific heat consumption — check the units and kiln configuration. A heat input of 750 kcal/kg clinker is approximately 3,140 MJ per metric tonne of clinker (3.14 GJ/t, or 3,140 kJ/kg), not 3,138 GJ/t. It is an illustrative operating value, not a universal guarantee for every suspension-preheater kiln. Compare actual fuel heat input on a consistent lower-heating-value basis per tonne of clinker and distinguish preheater-only from precalciner systems; moisture, fuel, cooler recovery and plant condition affect the result. The Cement Sustainability Initiative co-processing guidelines describe process-dependent thermal energy requirements.
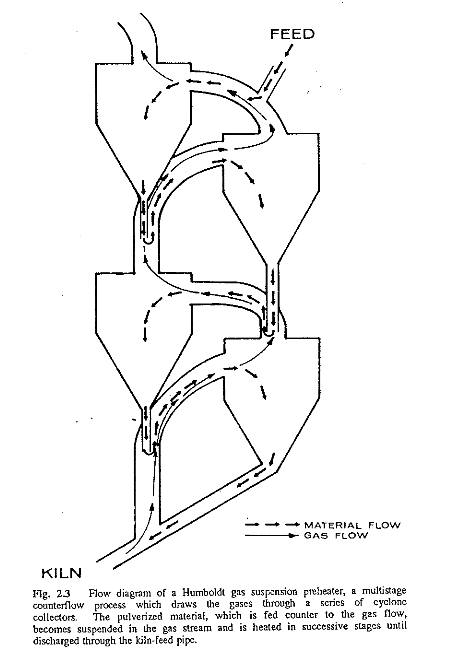
Fig. 2.3 Flow diagram of a Humboldt gas suspension preheater, a multistage counterflow process which draws the gases through a series of cyclone collectors. The pulverized material, which is fed counter to the gas flow, becomes suspended in the gas stream and is heated in successive stages until discharged through the kiln-feed pipe.
THE PRECALCINER KILN
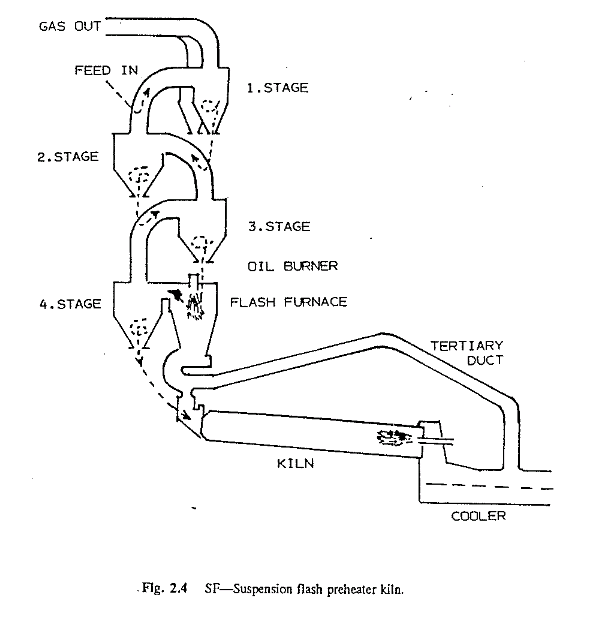
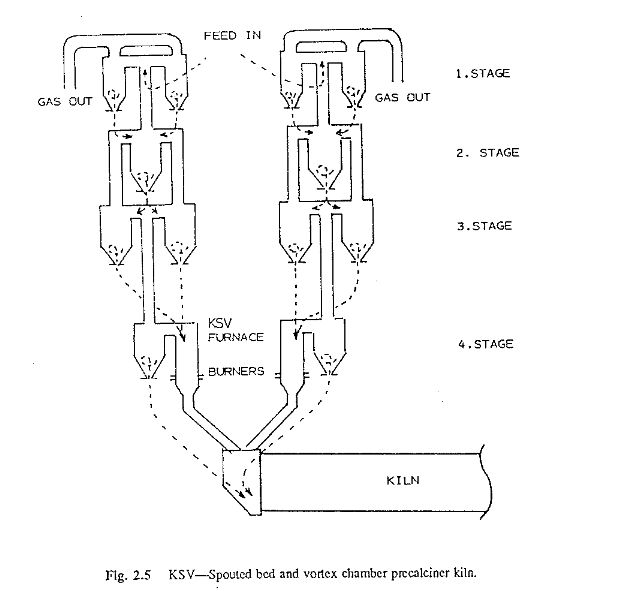
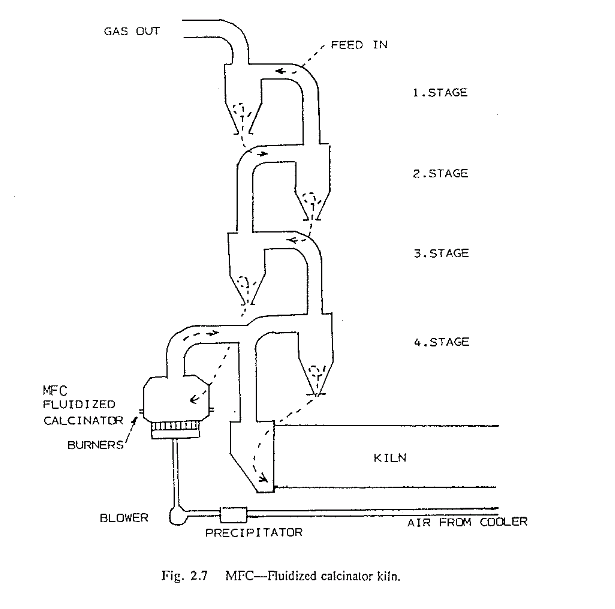
Roughly 15 years ago, Japanese cement manufacturers were confronted with the question of how best to increase the production rates of existing preheater kilns. As mentioned earlier, their preheater kilns reached limits in dimensions that gave rise to considerable operational and structural design problems. These kiln diameters became so large that refractory service life problems caused frequent and costly kiln down times. Then there was also the question of the possibility of using low-grade fuels in cement kilns that had to be addressed. Out of these considerations evolved the concept of auxiliary firing to precalcine the feed outside the rotary kiln. Pre calciners are essentially suspension preheater kilns that are equipped with a secondary firing system (commonly referred to as flash furnaces) attached to the lower stage of the preheater tower. This allowed kiln manufacturers to construct smaller diameter kilns without sacrificing kiln output, for a precalciner produces 50-70% more clinker than a conventional preheater kiln of equal diameter. A precalciner, however, does not operate at a lower specific total fuel consumption than a preheater kiln; their consumptions are approximately the same. But by burning 30-50% of the total energy input at the rear of the kiln, the heat load in the burning zone proper is reduced producing a beneficial effect on refractory service life. Aside from this, being able to use low-grade cheaper fuels in the auxiliary firing unit results in a reduction of the costs per unit weight of clinker. Therefore, although the energy consumption is the same, the cost for this energy is usually lower-a decisive factor in favor of the precalciner kiln.
There are two different types of precalciner kilns-kilns with tertiary air ducts and kilns without. As is discussed later in more detail, combustion of any type of fuel requires a given amount of air, hence this air has to be provided to the auxiliary firing unit at the back end of the kiln. This is done in two ways, either, the air comes from the kiln itself (no tertiary duct) or it is supplied by the enormous excess waste gases from the clinker cooler by means of the tertiary air duct that runs parallel to the kiln. Pre calciners without tertiary air ducts can be equipped with any kind of a cooler including planetary coolers whereas kilns with tertiary ducts cannot have planetary coolers. Kilns with tertiary ducts are more difficult to control for the operator since these kilns contain two distinct and separate combustion processes that must be closely controlled independently. However, the precalciner without the cooler air duct tends to be less efficient in fuel economy than the other when a large percentage of the kiln exit gases have to be bypassed in the preheater tower. Installation of a tertiary a’r duct is also very expensive and constitutes a high maintenance item. In the short time span of 90 years, rotary kilns have undergone vast changes. Great improvements in fuel efficiency and control technology have been made and most newly constructed kilns are fully automatic and controlled by computers. With a rating of 55%, the modern efficient cement kilns appear to have approached the limit of best attainable fuel efficiency and output. Have kiln manufacturers reached optimum kiln design? Is the precalciner kiln the kiln of the future? The author and many cement engineers do not think so. Technology has never stood still in an age of rapidly accelerating industrial changes. Cement kilns will not be exempted from this trend. Although the precalciner kiln is an important piece of process equipment, it has numerous shortcomings such as the enormity of the tall tower on the kiln backend, and problematic environmental conditions. Because these systems have become so sophisticated in matters of control and maintenance, well-trained specialists are now an absolute requirement. There are many new concepts for burning cement clinker that have been advanced by a multitude of forward thinking engineers. The fluid bed reactor, the separation of limestone calcining from other raw material preheating, the two-stage traveling-grate preheater are just some of the more “exotic” ideas that have come to the forefront. Perhaps one of these will be the kiln of the future, so it is important to keep an open mind toward such ideas and not regard them as “not possible.”
Frequently Asked Questions
What is a wet process kiln?
A wet process kiln is a type of rotary kiln where the kiln feed enters in the form of a slurry with a moisture content of 30 to 40%.
What is a semidry process kiln?
A semidry process kiln, also known as a Grate Process Kiln or Lepol Kiln, is a type of rotary kiln that is efficient in fuel consumption and has lower dust contents in waste gases.
What is a dry process kiln?
A dry process kiln is a type of rotary kiln where the kiln feed enters in dry powder form, with dimensions similar to wet kilns but without the need for an additional dehydration zone.
Need the kiln references in one engineering library?
Choose Engineering Essentials — $99 for the core engineering collection, or the Complete 931-File Package — $249 for the full kiln, pyroprocess, maintenance, troubleshooting and calculation library. Instant download immediately after successful payment. Confirm the final checkout amount before paying.
Next technical steps for rotary-kiln engineers
Need the complete kiln systems reference? Get operation guides, troubleshooting references, calculation tools and training material for kiln and pyroprocess work.
Start with Engineering Essentials — $99 or choose the Complete 931-File Package — $249. Instant download immediately after successful payment. Check the final price at checkout before purchasing.
I am working in acc cement wadi I need the job for fls plant
it was great explanation
it was good presentation
Pingback: Types of Rotary Kilns in Natural Graphite Anode Material Production: A Comprehensive Guide - ZDZN | Anode Material Production Line Specialist | EPC Engineering & Equipment Solutions