Separate mechanical vane hysteresis from a control-loop problem without masking the fault with tuning changes.
Capture command, feedback, actual vane angle or linkage motion, fan current and process draft in both stroke directions.
Repair backlash, binding, synchronization or feedback defects first; evaluate PID tuning only after the mechanical path is repeatable.
As-found evidence capture
Before adjustment, record operating mode, vane command, position feedback, observed linkage/blade position, fan current and controlled draft at repeatable points in both directions. Photograph or mark loose arms, worn pins, lagging vanes, stop contact and any binding. Preserve these readings as the before-repair baseline.
What inlet guide vane hysteresis means
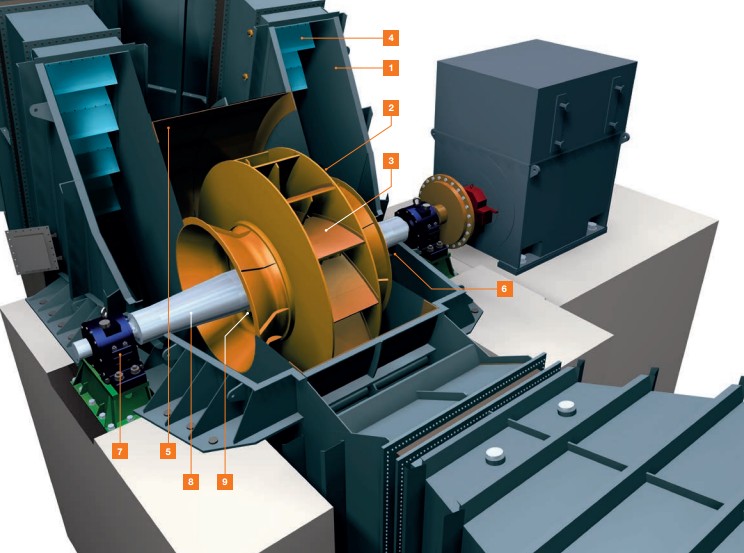
ID fan inlet guide vane hysteresis occurs when the commanded vane position and the actual mechanical vane position do not follow each other consistently. The same 40% command may produce different real vane angles depending on whether the actuator approached from opening or closing. Typical causes include linkage backlash, worn pins, loose arms, actuator deadband, binding blades, position-feedback error or poor synchronization between vanes.
Do not treat the problem as a process-control tuning issue until the mechanical position path is proven. Compare command, feedback and process response while stroking the vanes in both directions.
Why guide-vane hysteresis matters in cement plants
The ID fan controls a critical part of kiln and preheater gas flow. If inlet vanes respond differently when opening and closing, draft control can hunt, fan current can vary unnecessarily and operators may compensate with unstable set-point changes. A mechanical deadband can therefore look like a control-loop tuning problem while the real fault sits in the actuator, linkage or vane mechanism.
How to diagnose guide-vane hysteresis
Trend vane command, actual position feedback, ID fan motor current and the controlled draft signal together. Then stroke the vanes slowly from a lower position to a higher position and back down through the same set points. If actual vane position or draft response differs depending on direction, mechanical backlash, actuator deadband, feedback error or vane binding is likely. Use the installed fan and actuator OEM procedure for final stroke limits and calibration.
Key technical checks
- Verify the position transmitter or actuator feedback before assuming the displayed vane position is mechanically correct.
- Inspect actuator arm, clevises, pins, keys, splines and connecting rods for backlash or lost motion.
- Check whether all inlet guide vanes move together through the full stroke without one blade lagging or binding.
- Inspect pivot shafts, bushings and vane edges for dust buildup, corrosion, deformation or rubbing.
- Compare command-versus-feedback while opening and closing through the same positions to quantify deadband.
- Check actuator air/oil supply, positioner response, limit stops and calibration according to the installed actuator design.
- Correlate vane position with fan current and process draft so the mechanical correction is verified by actual fan response.
Common diagnostic mistakes
- Tuning the draft PID before proving that commanded vane position equals actual mechanical position.
- Calibrating the position transmitter while linkage backlash or a loose actuator arm is still present.
- Checking only one vane and assuming all linked blades move synchronously.
- Forcing a stiff vane mechanism with a stronger actuator instead of correcting binding or worn pivots.
- Testing only in one direction and missing the difference between opening and closing response.
- Accepting a stable feedback signal without verifying the actual vane angle and fan-process response.
Guide-vane hysteresis decision matrix
| Observed pattern | Check first | Likely direction |
|---|---|---|
| Command changes but feedback stays flat, then jumps. | Actuator positioner, linkage backlash, binding. | Deadband or lost motion. |
| Feedback moves smoothly but draft response is delayed. | Actual blade angle, vane synchronization, duct/process condition. | Feedback does not represent real vane movement. |
| Opening and closing give different draft at the same indicated position. | Pins, arms, pivots, blade binding. | Mechanical hysteresis. |
| One vane lags while others move. | Connecting rods, individual pivots, blade obstruction. | Synchronization fault. |
| Position is repeatable but control still hunts. | Process disturbance and control tuning. | Mechanical path likely healthy; review loop/process. |
Practical troubleshooting sequence
- Trend command, position feedback, fan current and controlled draft during stable operation.
- Stroke the inlet guide vanes slowly upward through several positions and record actual response.
- Repeat the same positions while closing the vanes and compare the two paths.
- During safe isolation, inspect actuator arms, pins, keys, connecting rods and vane pivots for lost motion or binding.
- Verify all vanes are synchronized and no blade reaches a stop early.
- Correct mechanical backlash or binding before recalibrating the feedback transmitter or positioner.
- After correction, repeat the opening/closing test and confirm similar draft and fan-current response at the same vane positions.
Frequently Asked Questions
How do you prove inlet guide vane hysteresis?
Command the same vane positions while approaching from opening and closing directions. If actual mechanical position or draft response differs materially at the same command, hysteresis or deadband is present.
Can the position feedback look normal while the vanes are wrong?
Yes. A transmitter may follow the actuator shaft while lost motion exists farther downstream in linkage pins, rods or individual vane pivots. Compare feedback with actual blade movement.
How can you separate PID tuning from a mechanical problem?
First prove repeatable mechanical position. If opening and closing produce the same actual vane angle and process response, then control-loop tuning and process disturbances can be evaluated more credibly.
What if only one guide vane lags?
Inspect that vane’s pivot, connecting rod, lever arm and local obstruction. One lagging blade can distort inlet flow even when the common actuator and feedback appear healthy.
What should be checked after linkage repair?
Repeat the full opening and closing stroke, verify synchronized vane movement, compare command with feedback, and confirm fan current and controlled draft respond consistently at repeated positions.
Return-to-service acceptance
- Command and position feedback track consistently through the full operating range.
- Opening and closing through the same set points produce comparable actual vane positions.
- All linked vanes move synchronously without visible lag, binding or early stop contact.
- Actuator arms, pins, rods, keys and pivots are secure with no abnormal lost motion.
- Fan current and controlled draft respond repeatably at repeated vane positions.
- The final linkage condition and position calibration are recorded as the new baseline.
Related Infinity technical guides
Use these references together with the installed fan and actuator OEM manuals; OEM stroke limits, calibration instructions and plant known-good baselines govern final acceptance.