Quick engineering answer
Kiln girth-gear backlash must be judged together with radial/axial runout and tooth-contact pattern. Measure repeatable circumferential stations, correlate backlash changes with runout, and do not move the pinion to chase one local reading while eccentricity or edge contact remains unexplained.
Establish repeatable kiln circumferential measurement stations.
Record backlash plus radial and axial runout at the same stations.
Check tooth contact, bearings, supports, fasteners and visible movement evidence.
Confirm the combined pattern meets the kiln and gear OEM limits before final alignment.
Measurement starting point
Use the kiln and gear manufacturer’s alignment procedure. Secure the drive, clean the tooth flanks and mark measurement positions around the circumference so readings can be compared at repeatable locations.
Measure backlash at several positions
Backlash is the clearance between mating tooth flanks. Measure it at multiple circumferential positions rather than at one point only. Record kiln position, pinion location and the measurement method so future shutdown inspections can be compared with the same reference.
Do not apply one generic backlash value to every kiln. The acceptable range depends on module, tooth geometry, gear diameter, mounting arrangement, operating temperature and OEM design.
Check radial and axial runout
Runout changes the effective centre distance and therefore changes tooth clearance around the rotation. Flender’s girth-gear instructions use dial-gauge measurements at multiple circumferential points to evaluate radial and axial runout. Excessive runout should be corrected before treating backlash alone as the primary defect.
Check the tooth contact pattern
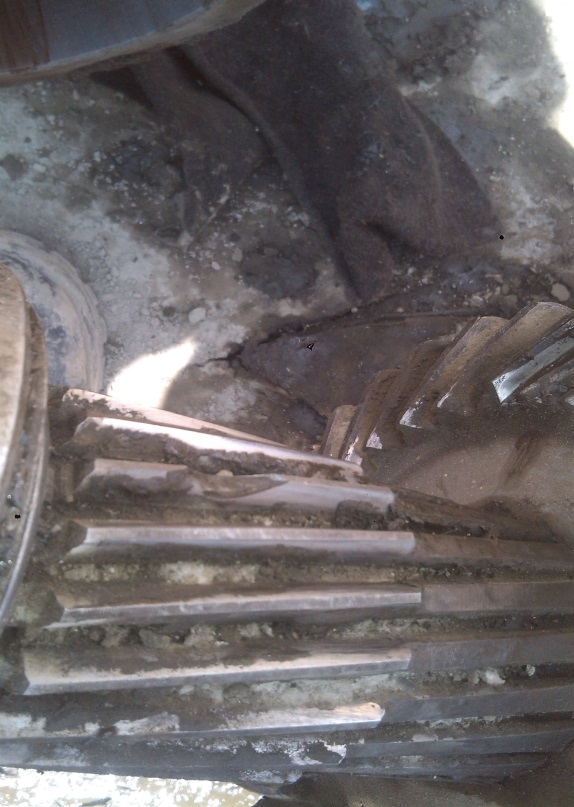
Inspect how the pinion contacts the girth gear across the tooth face. Uneven edge contact can indicate an alignment problem even when a single backlash reading looks acceptable. Record the contact pattern and compare it with previous shutdown inspections.
Interpret the measurement pattern
- Backlash changing strongly around the circumference: check runout or eccentricity.
- Low backlash with edge contact: check alignment and centre distance.
- Acceptable backlash with poor contact: check axial alignment and pinion angle.
- Progressive change between shutdowns: investigate wear or movement of supports.
Shutdown measurement sequence
- Clean the gear teeth and remove material that can distort the contact pattern.
- Mark repeatable circumferential measurement stations.
- Measure backlash at each station using the same method and reference flank.
- Measure radial and axial runout before interpreting backlash variation.
- Check tooth contact across the face width and note edge-loading patterns.
- Inspect pinion bearings, baseplate, fasteners, supports and visible movement marks.
- Compare the pattern with the kiln OEM limits and previous shutdown records.
Use a repeatable measurement worksheet
A single number cannot show whether the mesh is stable around the full rotation. Use a worksheet that keeps kiln position, backlash, radial runout, axial runout and tooth-contact observations together. Flender installation guidance for large girth gears uses dial-gauge readings at multiple circumferential positions and records the results so alignment can be evaluated as a pattern rather than a spot measurement.
| Station | Backlash | Radial runout | Axial runout | Contact observation |
|---|---|---|---|---|
| Reference position | Record | Record | Record | Centered / edge contact / irregular |
| Quarter rotation | Record | Record | Record | Compare with reference |
| Half rotation | Record | Record | Record | Compare with reference |
| Three-quarter rotation | Record | Record | Record | Compare with reference |
Use as many stations as the equipment manufacturer’s procedure requires. The important point is repeatability: use the same marked locations and method during future shutdowns so changes can be trended.
How to separate likely causes
| Measurement pattern | Diagnostic direction |
|---|---|
| Backlash varies with kiln rotation and follows runout | Investigate gear eccentricity, mounting or shell/gear runout before changing pinion position. |
| Backlash is comparatively stable but contact is concentrated at one edge | Investigate axial alignment, pinion angle, bearing/support condition and drive-train alignment. |
| Backlash changes after support or bearing work | Re-check centre distance and drive alignment against the OEM procedure. |
| Contact pattern and backlash progressively deteriorate between shutdowns | Investigate support movement, bearing condition, fastener condition, wear and structural movement. |
Do not correct backlash in isolation
Moving the pinion to obtain a preferred clearance can hide the real problem if the girth gear has excessive runout or the tooth contact is poor. Correct the root alignment condition first, then verify backlash again around the circumference. Never force the mesh toward zero clearance; OEM instructions for girth-gear units specifically warn that inadequate tooth-flank clearance can damage the gear.
Reference basis
Flender girth-gear installation guidance uses dial-gauge measurements at multiple circumferential points to evaluate runout and requires the readings to be recorded. FLSmidth’s cement services catalogue lists tooth condition, tooth contact, alignment, run-out and rotary backlash together in its gear-inspection scope.